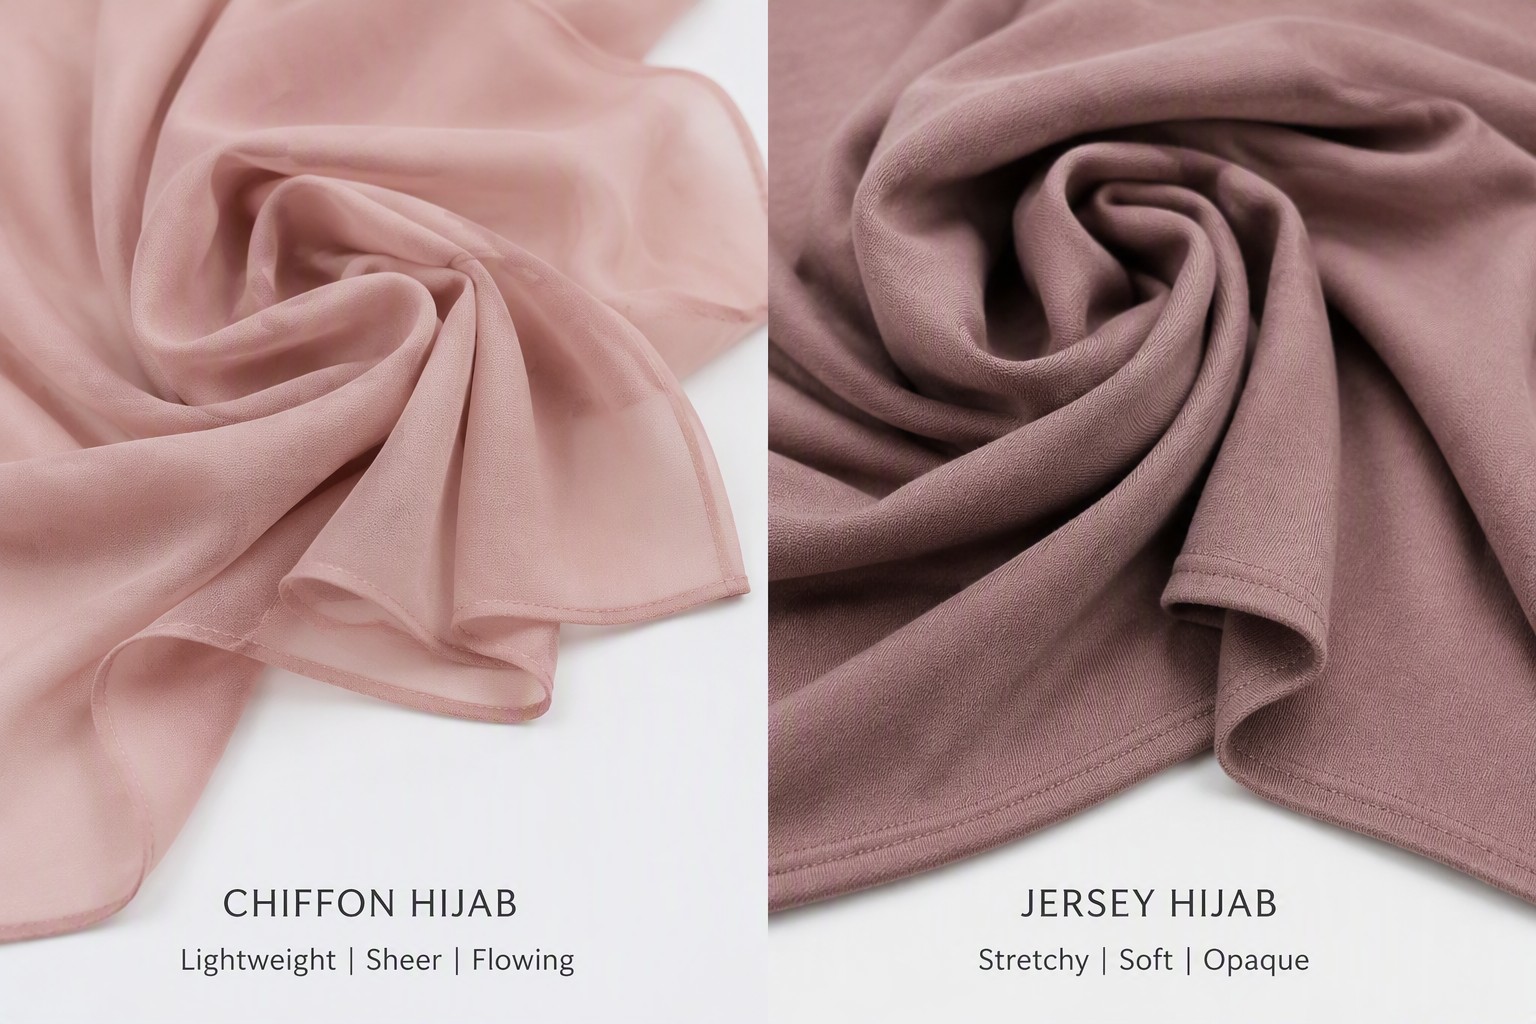
Quick Summary
A capable custom hijab manufacturer is distinguished from an assembly operation by equipment configuration decisions that determine whether print colour, construction dimensions, and wash-fastness can be replicated consistently across a production run and across repeat orders. The three equipment-critical variables in custom hijab production are ink delivery precision, fixation temperature consistency, and fabric tension management during cutting -- each of which has a specific failure mode that produces quality variation undetectable at the sample stage. Our production facility operates digital reactive print systems with closed-loop ink delivery feedback, fixation equipment calibrated to plus or minus 1.5 degrees Celsius, and a mandatory fabric relaxation protocol before cutting, which together provide the operational basis for consistent custom hijab output. Brands that arrive with defined quality standards -- colour references, dimension tolerances, wash-fastness grades -- rather than general quality expectations can use this equipment specification as a concrete basis for evaluating whether our production capabilities match their product requirements.
Introduction: What Separates a Capable Custom Hijab Manufacturer From an Assembly Operation
Custom hijab manufacturing is a technically demanding production process that requires more than cutting, sewing, and packaging fabric. The custom element -- whether that means a specific print design, a particular fabric weight, a branded label system, or a construction specification -- introduces variables that must be managed at the equipment level, the process level, and the quality verification level. A manufacturer that is equipped to manage these variables consistently is operationally different from an assembly operation that can produce volume but cannot reliably replicate a specific approved standard.
This product guide examines the equipment infrastructure that underpins reliable custom hijab manufacturing: the digital print system configuration, the fixation parameter management, the tension control during printing and cutting, and the outgoing inspection process that verifies the finished product against the approved specification. We also explain the practical implications of each equipment decision for a brand that is evaluating whether a manufacturer can deliver consistent results across the production run and across repeat orders.
Part 1: Buyer Problem -- Why Equipment Limitations Cause Custom Hijab Manufacturing Failures
Most custom hijab manufacturing failures that brands experience are equipment-related, not workforce-related. The factory workers may be experienced and attentive, but if the print equipment cannot maintain consistent ink delivery across a long run, if the fixation system cannot hold temperature within the tolerance required by the ink chemistry, or if the cutting system cannot hold dimensional tolerance on stretch fabric, quality variation is built into the production process regardless of worker skill.
The most common equipment-related failure in custom hijab manufacturing is print colour variation within a single production run. This occurs when the ink delivery system lacks precision feedback -- when the print head deposits ink at a rate that varies slightly across the run without automatic compensation. On plain fabric, this variation may be undetectable. On a custom print design, the variation manifests as visible colour difference between pieces produced at the start of the run and pieces produced at the end, which creates a batch that cannot be presented as a consistent product.
The second common failure is dimensional variation after washing. Custom hijab construction involves sewing on stretch fabric, which requires controlled tension at the cutting stage to ensure that cut pieces do not retract or distort after the tension is released. A cutting system that does not manage fabric tension during cutting will produce pieces that are dimensionally correct immediately after cutting but vary after washing, which is when the tension-induced distortion releases. This failure mode is difficult to detect at the pre-shipment inspection stage because the variation only becomes visible after the first wash cycle.
The third common failure is fixation temperature inconsistency, which affects wash-fastness rather than immediate colour appearance. Reactive ink on modal and jersey fabric requires precise fixation temperature and dwell time to complete the chemical bond between the ink and the fibre. If the fixation temperature is below specification, the ink bond is incomplete, and the colour fades more rapidly on washing than the approved standard indicates. This failure is not detectable in the outgoing inspection because the colour appears correct before washing; it only becomes apparent when the brand's end customers wash the product.
Part 2: Industry Trend -- Brands Are Specifying Equipment Requirements in Their Supplier Briefs
A growing segment of professional hijab brands has begun including equipment specifications in their supplier briefs alongside the product specifications. Rather than specifying only the desired output -- a colour, a dimension tolerance, a wash-fastness grade -- these brands are specifying the process parameters that are necessary to achieve that output reliably: digital print system type, fixation method, ink chemistry, tension control protocol. This shift reflects accumulated experience with manufacturing partners whose output quality was inconsistent because their equipment was not appropriate for the production requirements.
The brands that specify equipment requirements are typically those that have been through at least one significant manufacturing failure and have diagnosed the root cause at the equipment level. They have learned that a factory can produce a good sample under any conditions because the care taken with a sample can compensate for equipment limitations. They have also learned that bulk production under those same equipment limitations, where the care-per-unit is lower, produces results that differ from the sample in ways that are directly traceable to the equipment.
For brands that have not yet reached this level of technical specification, the equivalent filter is to ask manufacturers to describe their print system, their fixation system, and their tension control protocol in concrete terms. A manufacturer that can answer these questions with specific parameters -- print head type, fixation temperature range, tension measurement method -- has the process awareness that correlates with consistent production quality. A manufacturer that responds with general capability claims without specific process parameters is unlikely to have the operational discipline that consistent custom production requires.
Part 3: Technical Knowledge -- The Equipment Parameters That Determine Custom Hijab Quality
Digital reactive printing on modal and jersey hijab fabric involves three equipment-sensitive process stages: ink delivery, fixation, and tension management. Each stage has specific parameters that must be controlled within defined tolerances for the finished product to meet the approved standard consistently.
Ink delivery: digital textile printers deposit reactive ink at rates measured in grams per square metre. The target ink delivery rate for a given design is determined during the colour development stage and is recorded in the process specification for that design. During production, the printer must maintain this delivery rate within a tolerance of approximately plus or minus 3 percent to hold colour within the accepted delta-E range. Printers that lack automatic ink delivery compensation require manual monitoring and adjustment during the run, which introduces operator-dependent variation. Printers with closed-loop ink delivery feedback can maintain delivery consistency across longer runs with lower operator intervention.
Fixation: after printing, the reactive ink must be fixed to the fibre through a steaming or heat fixation process. For modal fabric, steam fixation at 102 to 105 degrees Celsius for 8 to 12 minutes is the standard range; for jersey fabric, the fixation temperature is typically higher and the dwell time shorter due to the synthetic fibre content. Fixation equipment that holds temperature within plus or minus 2 degrees Celsius across the full width of the fabric and along the full length of the fixation chamber produces consistent wash-fastness results. Equipment that allows temperature variation outside this range produces inconsistent fixation, which shows as uneven wash-fastness across a batch.
Tension management: modal and jersey fabrics are stretch fabrics that respond to tension by elongating and then retracting when tension is released. A print run that applies uneven tension to the fabric during printing will produce design distortion that varies across the roll, because the distortion is proportional to the tension applied at each point. A cutting operation that holds the fabric under tension while cutting will produce pieces that retract after cutting, resulting in finished dimensions that are smaller than the cut dimensions. Our production process includes a fabric relaxation protocol that allows fabric to rest without tension for a defined period before cutting, which ensures that the cut dimensions correspond to the finished dimensions after washing.
Part 4: Our Factory Capability -- Equipment Configured for Custom Hijab Production Requirements
Our print production facility operates digital reactive print systems that have been configured specifically for modal and jersey hijab production requirements. The configuration choices -- print head arrangement, ink delivery system type, fixation chamber design, fabric feed tension control -- were made based on the specific characteristics of the fabrics and designs we produce rather than on general-purpose textile printing requirements.
Our print system operates with closed-loop ink delivery feedback that monitors and adjusts ink deposit rate continuously during the print run. This configuration maintains ink delivery within our accepted tolerance of plus or minus 2.5 percent of the target rate across the full production run, which is the operational basis for our colour consistency across long runs. We record the actual ink delivery data for each production run in the order file, which provides a traceable record of the process parameters used for each batch.
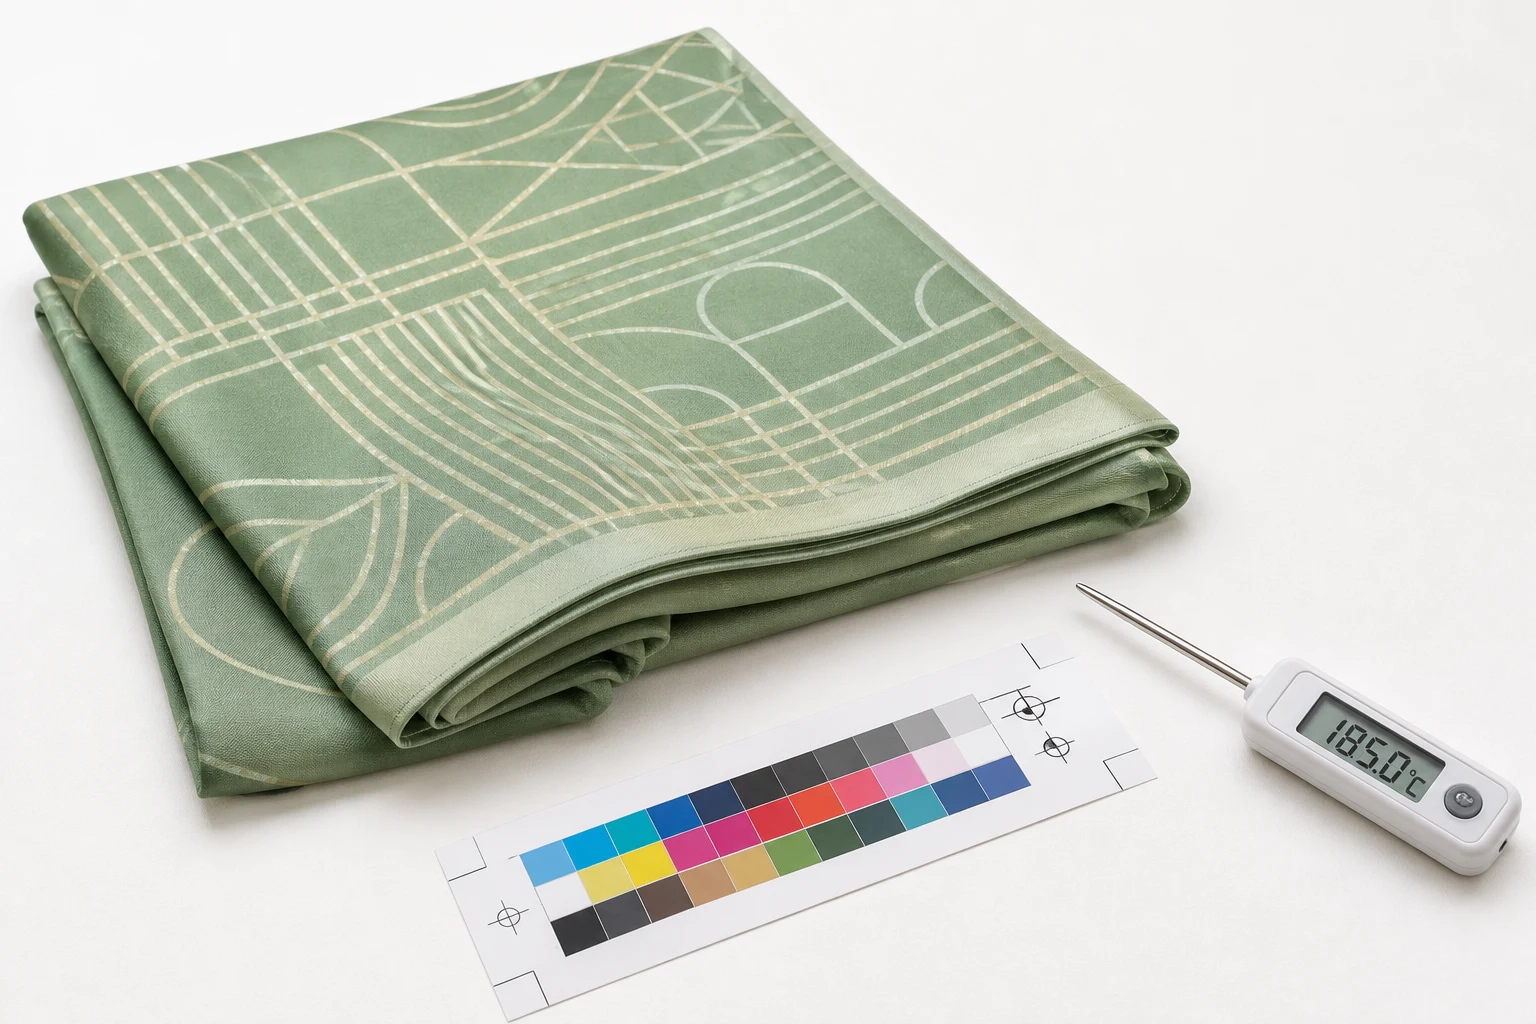
Our fixation system maintains steam temperature within plus or minus 1.5 degrees Celsius across the full fabric width and along the fixation chamber length. We verify fixation temperature at the start of each production day using calibrated temperature measurement, and we re-verify after any fixation chamber startup or adjustment. The temperature verification records are retained in the production log for each batch. Our fixation parameters for each fabric and ink combination are recorded in the design specification file and are applied consistently for all production runs using that design.
Our fabric handling protocol includes a minimum relaxation period for all modal and jersey fabric before cutting. Fabric rolls are unwound and allowed to rest on a flat surface without tension for at least four hours before the cutting process begins. This relaxation period allows the fabric to return to its natural dimensions, ensuring that cut dimensions correspond to the finished product dimensions after washing. We have measured the dimensional difference between immediately-cut pieces and relaxation-cut pieces on our standard fabrics, and we use the relaxation protocol as a non-negotiable step in our production process for all custom orders.
Part 5: Quality Control -- Outgoing Inspection Against the Approved Specification
Our outgoing inspection for custom hijab orders is conducted against the approved specification for each order, not against a general quality standard. The approved specification includes the colour standard (delta-E measurement against the approved strike-off), the construction dimensions (length, width, and hem width with tolerances), and the wash-fastness grade (ISO 105-C06 result for the approved design and fabric combination).
Colour inspection: we inspect 100 percent of finished units under D65 standard illuminant using a lightbox. Units that show visible colour deviation from the approved colour standard reference are set aside for spectrophotometric measurement. Units that measure outside delta-E 2.0 against the approved standard are rejected from the shipment and reprocessed. For orders where we have an approved strike-off on file, the strike-off is used as the physical colour reference during inspection rather than a printed colour specification, which eliminates the colour shift that can occur between screen or print representations and the actual fabric colour.
Dimensional inspection: we apply AQL 2.5 sampling for dimensional inspection, measuring length, width, and hem width on a statistically representative sample from each production lot. Measurements are taken at four points on each piece -- two length measurements at different positions across the width, and two width measurements at different positions along the length -- to detect both overall dimension variation and taper or distortion. Pieces that fall outside the specification tolerances are removed from the shipment. The dimensional inspection results for each lot are recorded in the shipment quality report that accompanies each order.
Wash-fastness verification: for new designs and for any order using a new fabric batch, we conduct a wash-fastness test on a production sample before releasing the shipment. The test follows ISO 105-C06 protocol at 40 degrees Celsius, and the result is compared against the approved wash-fastness grade for the design. If the production sample result falls below the approved grade, we investigate the cause -- typically a fixation parameter deviation -- before releasing the batch. For established designs on known fabric batches where previous wash-fastness results are on file, we use the incoming material dye affinity assessment result to confirm that the current fabric batch is consistent with previous batches, and release the shipment without a separate wash test.
Part 6: Brand Development Advice -- Specify Your Quality Standard Before You Brief a Manufacturer
The most effective way to use a custom hijab manufacturer is to arrive with a defined quality standard rather than a general quality expectation. A defined quality standard includes: the colour reference you will use to evaluate production samples (a fabric swatch, a Pantone reference, or a specific colour space value), the dimension tolerances you require for the finished product, and the minimum wash-fastness grade you need for your intended market and care instruction claim.
A manufacturer that receives a defined quality standard can tell you immediately whether their equipment and process configuration can meet that standard. A manufacturer that receives only a general quality expectation will produce the best output their current configuration can achieve and present it as meeting the brief -- because they have no basis to evaluate whether it actually meets an unstated standard. The difference between these two conversations is the difference between a sourcing process that identifies fit and one that discovers misfit after a bulk order has been produced.
If you are building a custom hijab programme and are ready to move from general quality expectations to defined quality standards, we can help you translate your brand requirements into specific production parameters. Share your current samples, your existing care instruction claims, and any quality issues you have encountered with previous manufacturers, and we will provide a gap analysis between your current standard and our production output -- along with a clear description of the production run we would propose to validate fit. This is the starting point for a supplier relationship built on specification rather than expectation.
Frequently Asked Questions
What print system do you use for custom hijab production?+
We operate digital reactive textile print systems configured specifically for modal and jersey hijab production. Our print systems use closed-loop ink delivery feedback to maintain ink deposit rate within plus or minus 2.5 percent of the target rate across the full production run. The specific print system model and configuration details are available on request during a supplier evaluation conversation.
How do you control fixation temperature consistency across a production run?+
Our fixation system maintains steam temperature within plus or minus 1.5 degrees Celsius across the full fabric width and along the fixation chamber length. We verify temperature at the start of each production day and after any chamber adjustment using calibrated temperature measurement equipment. Fixation parameters for each fabric and ink combination are recorded in the design specification file and applied consistently for all production runs using that design.
What is your AQL standard for outgoing dimensional inspection?+
We apply AQL 2.5 sampling for major dimensional defects during outgoing inspection. We measure length, width, and hem width at four points per piece on the sampled units to detect both overall dimension variation and taper or distortion. The dimensional inspection results for each production lot are recorded in the shipment quality report that accompanies each order.
How do you manage fabric tension during cutting to prevent dimensional shrinkage after washing?+
We require a minimum four-hour relaxation period for all modal and jersey fabric before cutting begins. During this period, the fabric rests on a flat surface without tension, allowing it to return to its natural dimensions. This protocol ensures that cut dimensions correspond to the finished product dimensions after washing. We have measured the dimensional difference between immediately-cut and relaxation-cut pieces and use the relaxation protocol as a non-negotiable production step for all custom orders.
What documents do you provide with each shipment?+
Each shipment is accompanied by a shipment quality report that includes: the colour inspection result (number of units inspected, number rejected, and the colour reference used), the dimensional inspection result (AQL sampling record and the specific measurements taken), and the wash-fastness test result for new designs or new fabric batches. For repeat orders, we also provide a comparison between the current batch measurements and the historical measurements for the same account, which allows the brand to verify consistency between orders.
What minimum order quantity do you accept for custom printed hijab production?+
Our minimum order quantity for custom printed hijab styles varies by fabric type and design complexity. For standard modal and jersey designs using established ink formulations, our minimum quantity is typically 150 to 200 pieces per colourway. For new designs that require a full colour development round, the minimum quantity may be higher to cover the development investment. We recommend discussing your specific design and timeline requirements during a briefing conversation so we can confirm the applicable minimum and production schedule.
Need a quote for your next order?
Free samples available. MOQ from 100 pieces. Ships to 50+ countries.
Request a Quote